 English
 Arabic
 Dutch
 French
 German
 Italian
 Portuguese
 Russian
 Spanish
An OEM purchase order that says only “stainless, passivated” leaves important questions unresolved. Which material is being supplied? Which treatment and verification requirements apply? What record connects the result to the delivered lot? This guide focuses on those decisions so the drawing, quotation and inspection record describe the same requirement.
What passivation does—and what appearance cannot prove
Passivation is a post-fabrication process that improves the corrosion resistance inherent in the selected stainless grade. Process planning should emphasize cleaning before treatment because an unsuitable process can itself damage the surface. Alloy-specific process selection matters; the treatment is not a way to turn one grade into another.
Keep material identification and treatment verification as two separate acceptance items. The material record establishes the specified alloy and any additional required properties. The treatment record addresses the approved surface process and its verification. Photographs can support visual inspection, but cannot identify an invisible passive film or prove a batch met an agreed test.
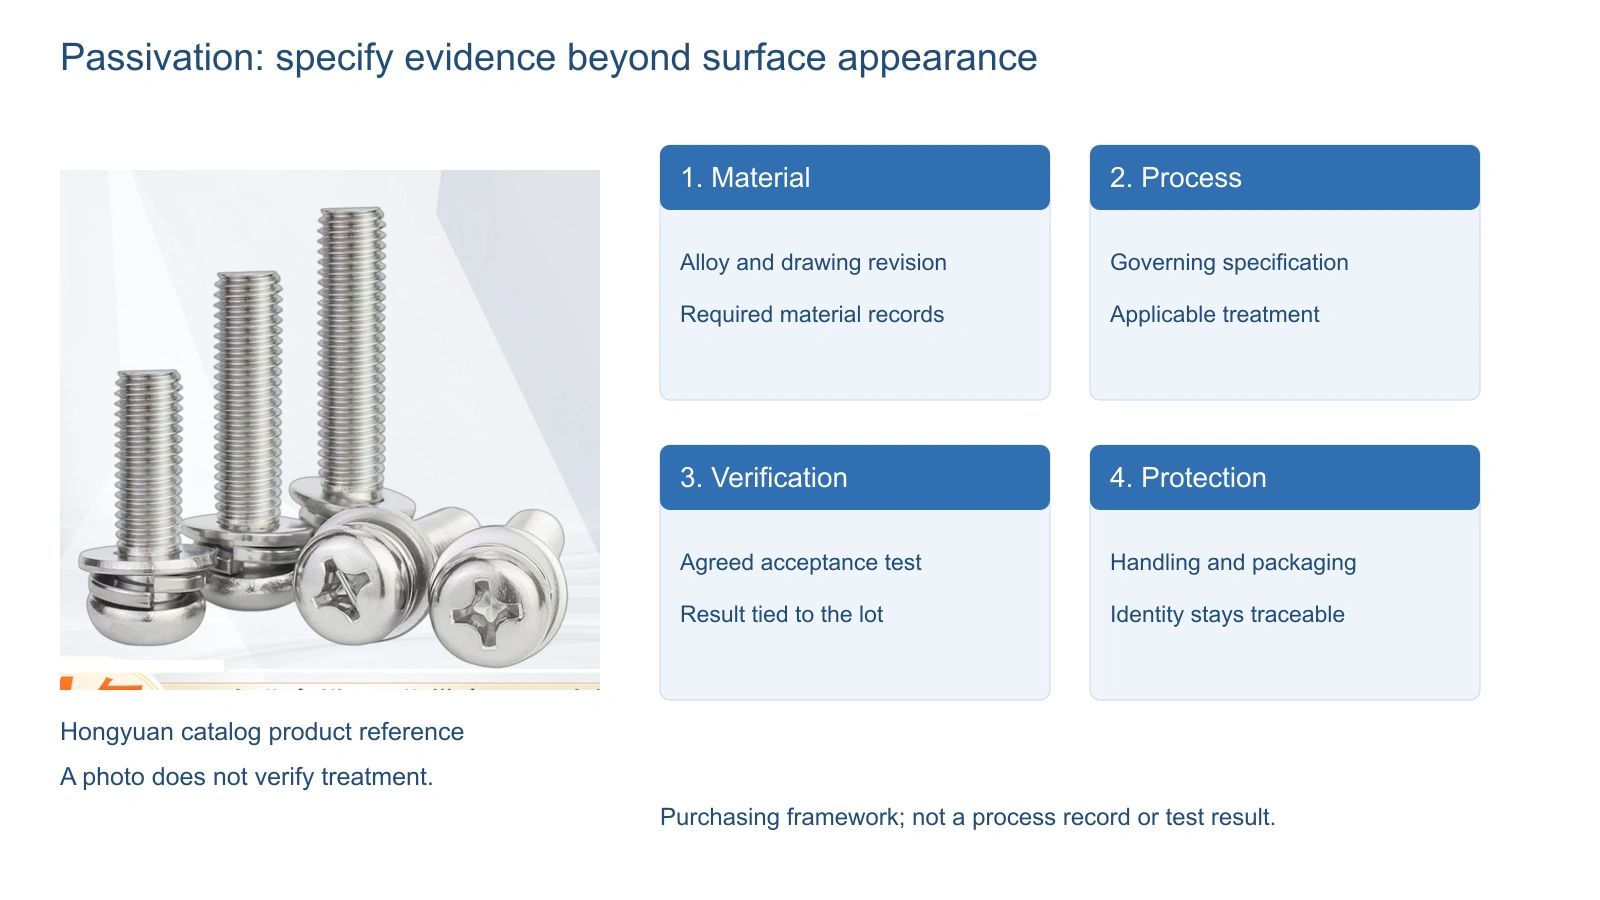
Cleaning, descaling and passivation are different requirements
| Requirement | Purpose in the enquiry | What should not be assumed |
|---|---|---|
| Cleaning | Define removal of oils and other unwanted residues | A visually bright surface is chemically clean |
| Descaling / pickling | Define removal of scale or other specified surface conditions | The word passivation includes every prior preparation operation |
| Passivation | Identify the agreed stainless surface treatment | The treatment changes the base alloy or guarantees lifetime |
| Separate coating / finish | Specify any independently required added finish | A coating request can be replaced by an unrelated surface process |
ASTM A380/A380M covers guidance for cleaning, descaling and passivation, including application-dependent cleanliness and protection against recontamination. Its public scope also notes that procedures may be agreed between purchaser and supplier. That supports a defined drawing requirement rather than an unspecified request to make screws “more corrosion resistant.”
Describe the starting condition that needs attention. Machining residue, handling contamination and heat-related scale are different concerns. Where the process provider needs to assess a sample, keep the condition identifiable and state whether the part has already received another finish. Avoid prescribing a chemical recipe from a general blog; this is a procurement guide, not an operating instruction.
How to reference ASTM A967 without losing the acceptance criteria
The public scope of ASTM A967/A967M identifies different chemical passivation treatments and alternative verification tests with acceptance criteria. Naming the standard does not eliminate the need to agree the applicable treatment, verification selection and documentation. Use the edition required by the contract, and review the actual specification for the alloy and application.
| Purchase-order item | Question to resolve before approval |
|---|---|
| Material | What alloy and material documentation are required? |
| Specification | Which standard, edition and applicable treatment requirements govern? |
| Verification | Which applicable test, acceptance criterion and sampling/lot definition are agreed? |
| Traceability | How will the report identify the supplied part and treatment lot? |
| Packaging | How will treated parts be handled and protected during shipment? |
| Additional requirements | Are dimensional checks, lubricant restrictions or application cleanliness requirements separate? |
Avoid copying a list of every available test into an order and calling the requirement complete. The selected method must be applicable, and the result must be interpreted using the agreed acceptance criteria. A short certificate saying “pass” is more useful when it identifies what was tested and the lot it represents. This article does not establish Hongyuan certification or a particular in-house laboratory capability.
An illustrative document review before shipment
Imagine an order for a defined stainless machine screw with an agreed passivation requirement. The buyer receives a material document, a treatment certificate and an inspection report. Review them as a connected package: do all three refer to the correct part revision, material and lot? Is the stated treatment the one agreed in the order? Does the inspection report name the verification basis instead of showing an unexplained pass mark? These are hypothetical review questions, not a Hongyuan customer result.
If a report and package label use different identifiers, resolve the link before accepting the paperwork. Record the discrepancy and request the missing connection rather than changing the identifiers to make them match. If a condition changes after approval, ask whether the existing evidence remains applicable to the revised lot or process.
Receiving inspection: separate three kinds of evidence
Use visual observations for what is visible, dimensional inspection for the specified geometry, and the agreed surface-verification record for the treatment requirement. Record these as separate fields. This keeps a scratched head, a thread-fit concern and a missing certificate from being merged into one unsupported conclusion about passivation.
For handling, define packaging cleanliness and any contamination restrictions appropriate to the application. Preserve part and lot identification when repacking. A passed verification record does not make subsequent uncontrolled storage irrelevant. If additional corrosion testing is requested, state the method and acceptance basis separately; do not convert a laboratory test duration into a promised number of service years.
Frequently asked questions
Can I recognize passivation from a shiny surface?
No. Surface appearance is not enough to establish treatment identity or compliance. Use the agreed process and verification records.
Does passivation make 304 equivalent to 316?
No. Keep the base material specification separate from the surface-treatment requirement. Treatment does not substitute for the alloy specified by the designer.
Does writing ASTM A967 mean every listed test must be ordered?
Do not infer that from a summary. Review the governing edition and agree the applicable verification requirements with the process provider and purchaser.
Should a passivation certificate replace dimensional inspection?
No. Geometry and the treatment requirement are separate acceptance items. The inspection plan should address each applicable requirement.
Build a complete Hongyuan finish enquiry
Send the drawing, alloy requirement, intended environment, applicable finish specification and requested documentation. Ask which process and verification arrangements can be evaluated for the proposed order, including any external process provider. Confirm that scope before placing the order rather than assuming capability from a general product photograph.
Related reading: How to Choose the Right Screw Surface Treatment. Contact Hongyuan with your drawing and purchasing requirements.